In industrial boiler water treatment, many factories are falling into the trap of low-cost consumables. They purchase seemingly inexpensive disposable filter elements, only to find that these filters need to be replaced every one or two weeks due to excessive differential pressure. When labor costs, production downtime, and waste filter disposal expenses are included, the actual operating costs become surprisingly high.
In biomass boiler feedwater pretreatment and circulating water side-stream filtration systems, impurity loads can fluctuate significantly, and operating temperatures are often relatively high. Conventional filter elements have limited dirt-holding capacity. Once clogged, they cannot be effectively restored and must be discarded, resulting in significant resource waste and additional supply chain pressure.
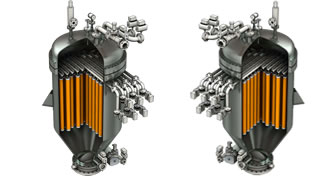
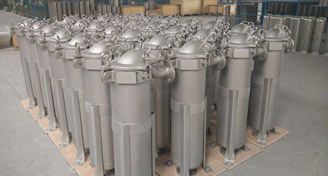
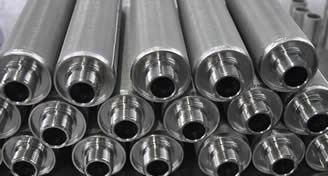
How can this problem be solved? One effective solution is to replace disposable consumables with reusable 316 stainless steel sintered mesh filter elements.
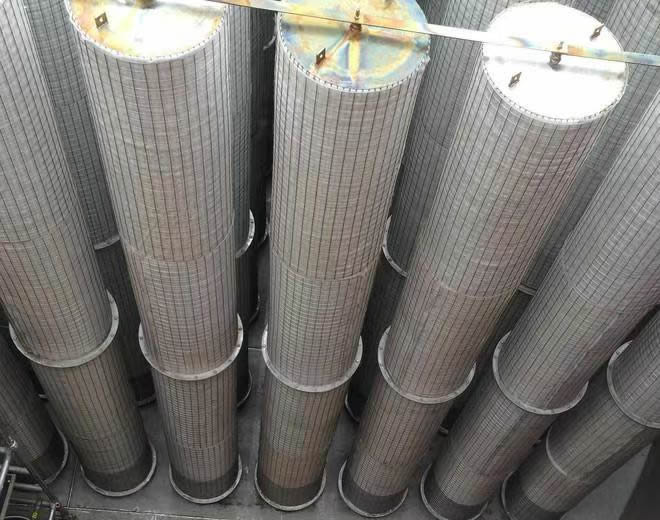
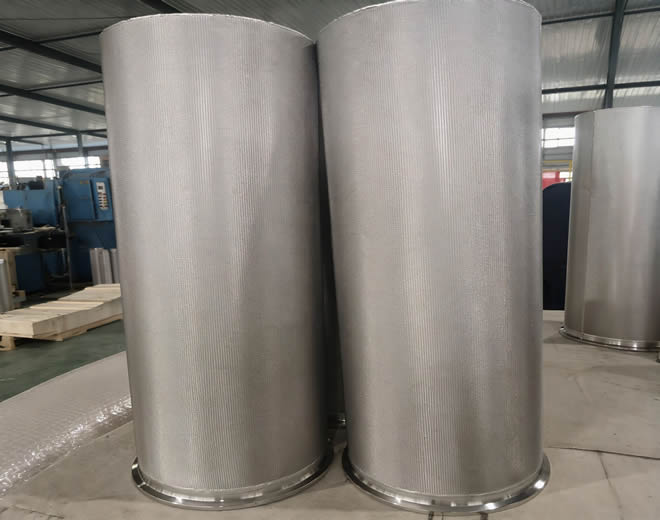
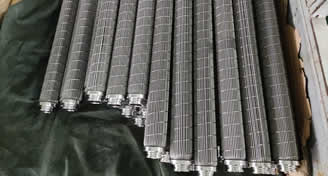
As a direct manufacturer, we produce five-layer and seven-layer 316 stainless steel sintered mesh filter elements using an integrated sintering process. The filtration layer is firmly supported by protective mesh layers on both sides, ensuring uniform pore distribution and reliable structural strength. Filtration ratings range from 2 to 200 microns.
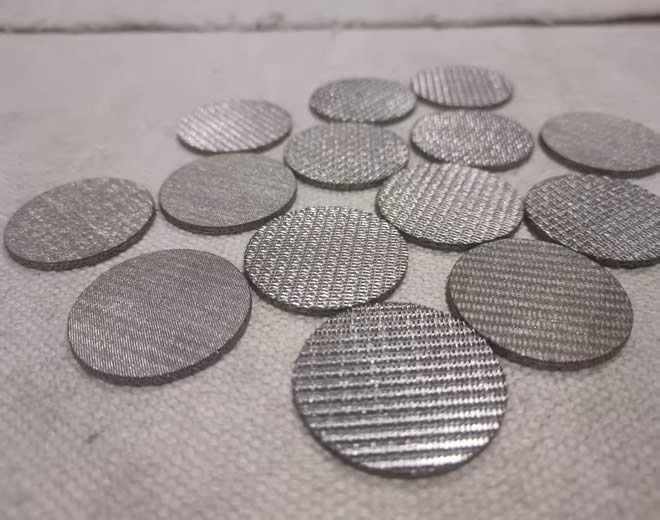
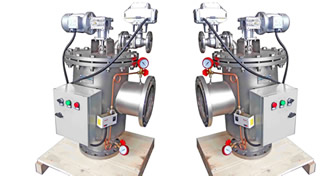
When accumulated particles cause the differential pressure to rise, the filter element does not necessarily need to be replaced. Through online system backwashing or scheduled offline chemical or ultrasonic cleaning, its initial flow capacity can be restored to over 95%, under suitable operating and cleaning conditions.
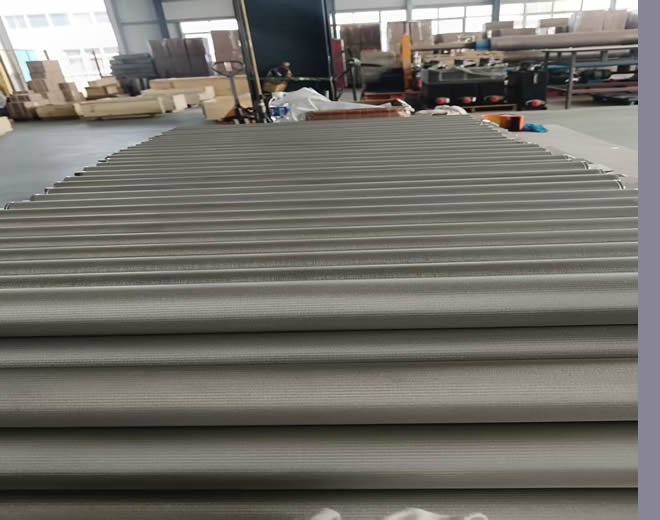
A high-quality 316 stainless steel sintered mesh filter element can have a service life of several years, depending on the actual operating conditions and maintenance practices. This can help industrial users reduce long-term filtration costs by more than 60%, while minimizing consumable waste and maintenance requirements.